
Leave Your Message
-
Contact WhatsApp
-
 Contact Phone
-
 Contact Email
Engineered to meet the stringent demands of the Permian Basin, Bakken, and Gulf of Mexico operations.

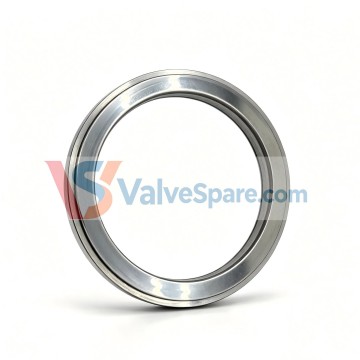

The United States oil and gas industry is characterized by some of the most challenging geological environments in the world. From the ultra-deepwater wells of the Gulf of Mexico to the high-volume hydraulic fracturing operations in the Permian Basin, the demand for reliable, high-performance flow control equipment has never been greater. At the heart of these critical systems is the API 6A gate valve, and more specifically, the API 6A valve seat. As a vital component responsible for ensuring a bubble-tight seal under pressures that can exceed 15,000 to 20,000 psi, the valve seat is the line of defense against catastrophic leaks, environmental hazards, and costly downtime.
API 6A specifications, set by the American Petroleum Institute, define the stringent requirements for wellhead and Christmas tree equipment. For valve seats, this means adhering to precise tolerances, advanced material sciences, and rigorous testing protocols. As leading manufacturers and suppliers serving the United States market, we specialize in delivering API 6A valve seats that meet and exceed these standards, providing American operators with the reliability they need to sustain safe and profitable operations.
The landscape of US oil and gas production has shifted dramatically over the past two decades. The shale revolution has turned the US into a leading global oil and gas producer. However, extracting resources from shale formations requires multi-stage hydraulic fracturing and horizontal drilling, techniques that subject surface and subsurface valves to extreme stress. Frac manifolds and flowback systems handle fluid mixtures containing high concentrations of abrasive sand (proppants), corrosive chemicals, and high-velocity hydrocarbons. Under these conditions, standard valves degrade rapidly. The API 6A valve seats used in these systems must possess exceptional wear resistance to withstand the continuous bombardment of abrasive particles.
In offshore regions like the Gulf of Mexico, the challenges are different but equally severe. Deepwater wells operate under high hydrostatic pressures and are exposed to highly corrosive marine environments. The costs associated with replacing a failed valve seat in a subsea Christmas tree are astronomical. Consequently, operators demand valve seats crafted from high-performance alloys and coated with state-of-the-art thermal sprays, such as Tungsten Carbide or Cobalt-based alloys, to guarantee long-term operational integrity. Our supply chain is structured to deliver custom-engineered API 6A valve seats directly to these active basins, ensuring that project timelines are maintained without compromising on component quality.
The US energy market is undergoing a technological transformation driven by digitalization, efficiency optimization, and ESG (Environmental, Social, and Governance) commitments. One of the most prominent trends in valve manufacturing is the adoption of advanced surface modification technologies. Supersonic flame spraying, specifically High-Velocity Oxygen Fuel (HVOF) and High-Velocity Air Fuel (HVAF) methods, has become the industry standard for applying hard coatings to API 6A valve seats and gates. Utilizing equipment like the PRAXAIR TAFA JP8000 allows us to apply dense, low-porosity coatings of Tungsten Carbide (WC-Co-Cr) that dramatically extend the service life of valve components in high-abrasion environments.
Another major trend is the reduction of fugitive emissions. The US Environmental Protection Agency (EPA) has implemented strict regulations regarding methane leaks from oil and gas infrastructure. Because gate valves are common points of potential leakage, the sealing interface between the gate and the seat must remain perfectly tight over thousands of cycles. This has driven the industry toward metal-to-metal sealing technology. Unlike soft seals, which can degrade or blowout under high pressures and temperatures, metal-to-metal seats rely on ultra-precise surface finishes (often lapped to within light-band tolerances) to prevent gas molecules from escaping. Our manufacturing processes focus heavily on achieving these micro-inch finishes, directly supporting US operators in meeting their net-zero and emission-reduction targets.
API 6A valve seats find critical applications in several key areas across the US oilfield infrastructure:
In today's era of convenient internet communication, trust is scarce. We have always stayed true to our original aspiration, crafting valve products with meticulous craftsmanship, and winning recognition from global buyers.
Founded in 2011 in a humble workshop in Suzhou, our core mission was to break the monopoly of foreign high-end valve plates and seats, so that buyers would no longer have to rely on overpriced imported products. Facing industry pain points such as seat seal leakage and high-sulfur corrosion in oilfield applications, we stayed rooted in frontline operations, braving high temperatures and pressures to repeatedly test materials and optimize sealing structures, successfully resolving leakage issues.
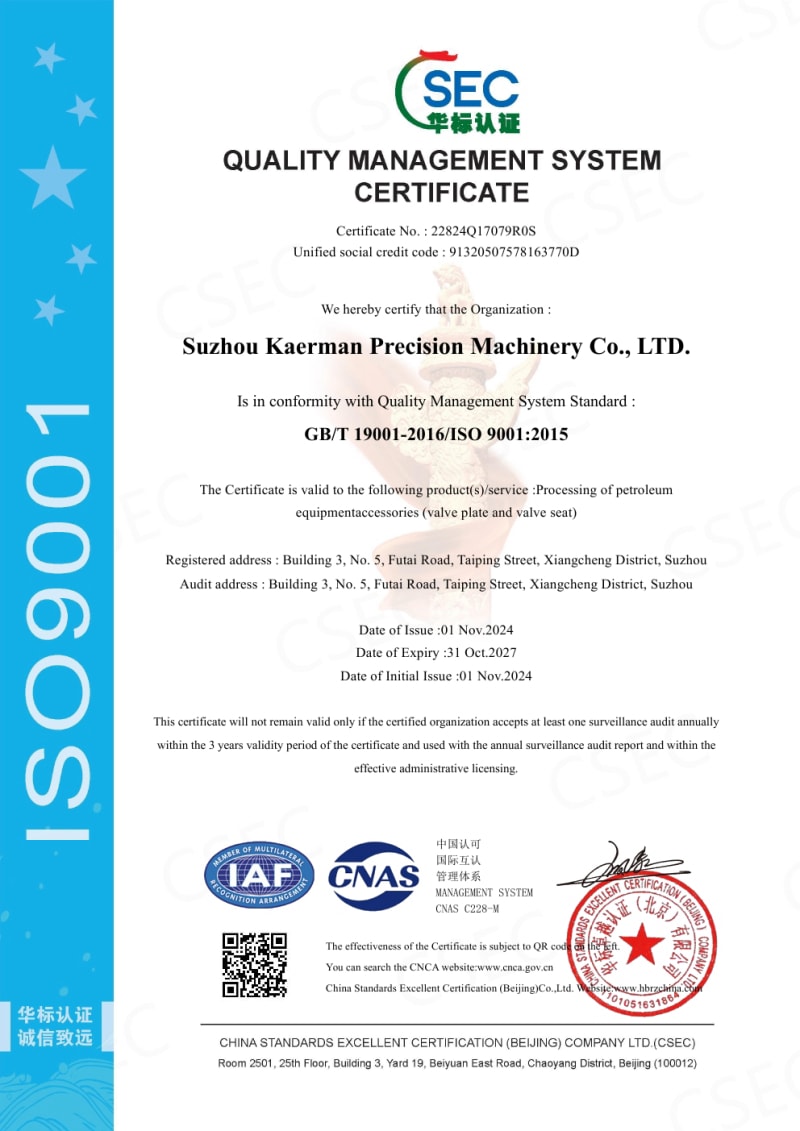
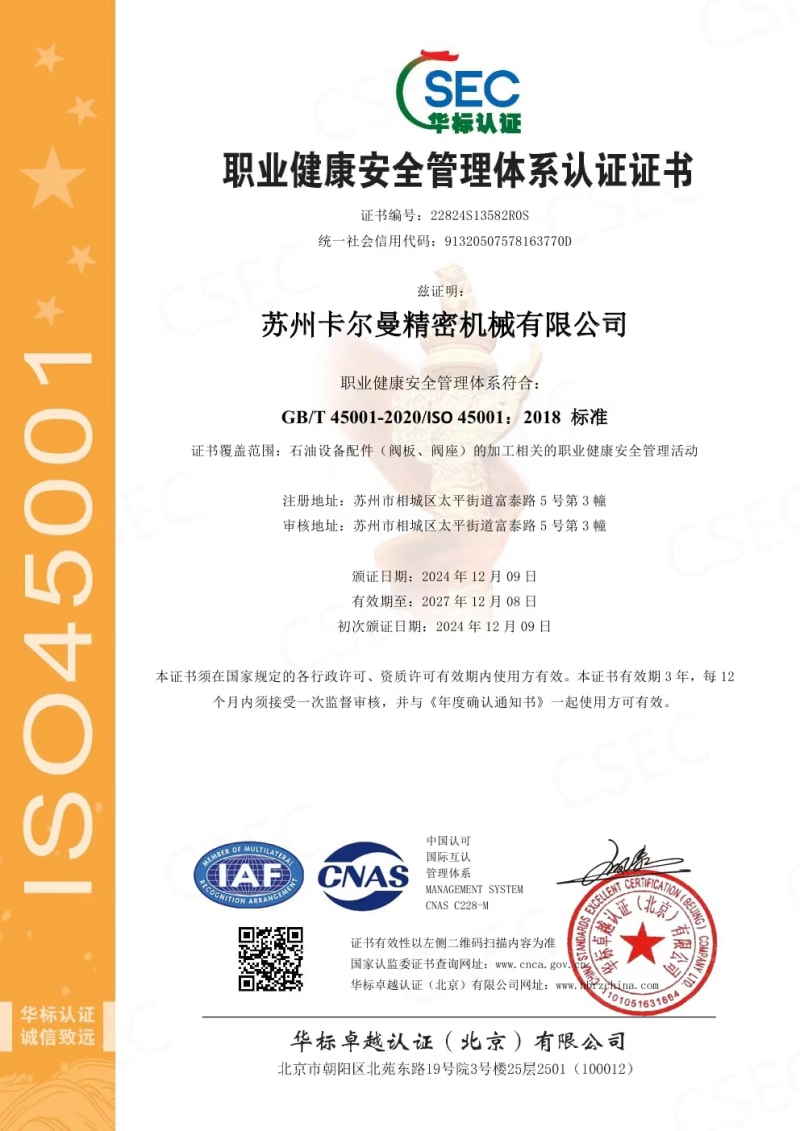
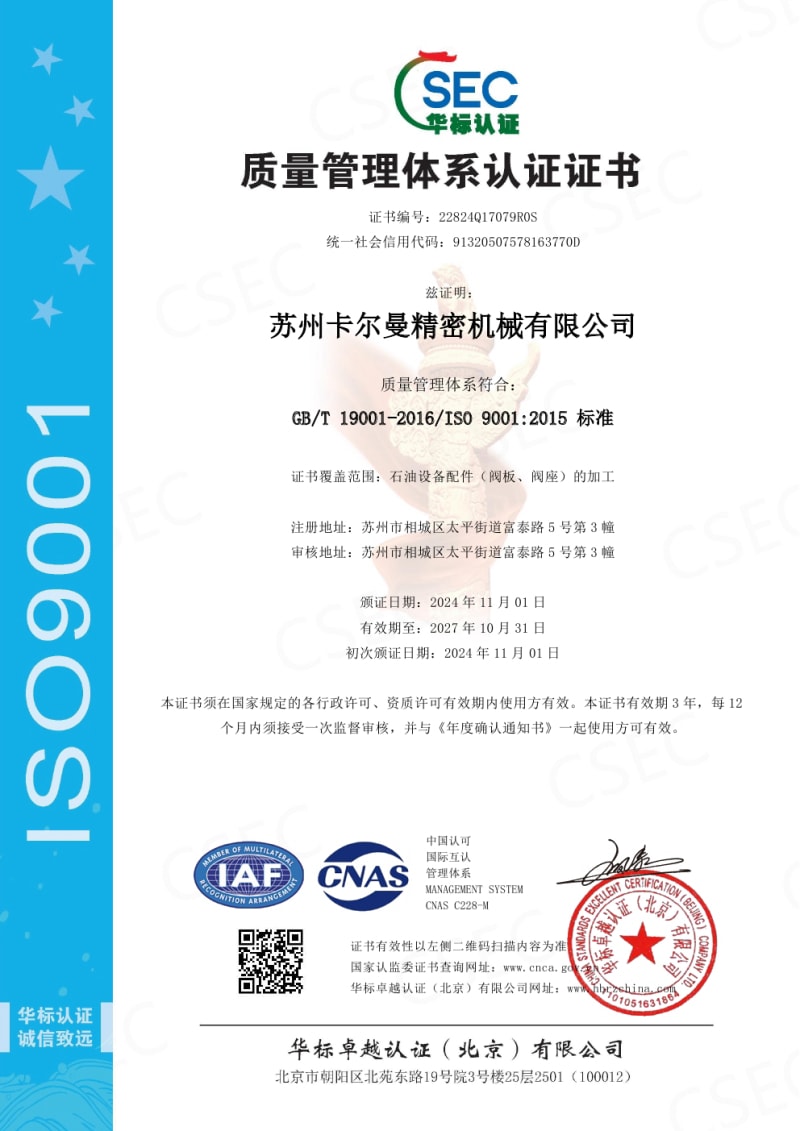
We are deeply committed to quality and have obtained API certification as well as the three management system certifications. From developing only valve plates and seats, we have grown into a partner capable of providing comprehensive solutions.
After 15 years of perseverance, we uphold our original aspiration with craftsmanship, and have become a trusted supplier of high-end valve accessories for global buyers through professionalism and sincerity.
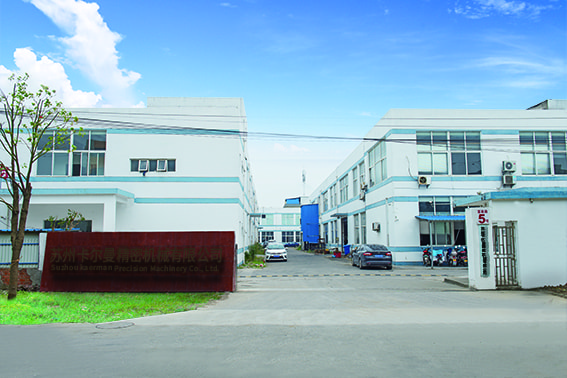
We are a team of seasoned engineers and technicians with years of hands-on experience in supersonic flame spraying for petroleum machinery. All core operators receive systematic professional training, bringing deep expertise in thermal spray technology and quality control.
We specialize in manufacturing precision wear-resistant parts (including valve gates, wellhead components, and sealing parts) using advanced PRAXAIR TAFA JP8000 supersonic flame spraying equipment. We customize coating processes and parameters for different products to deliver exceptional performance under extreme working conditions.
Our operational scale and technical certifications ensure reliable supply chain performance for our US partners.
We solve critical pain points for oil & gas operators:
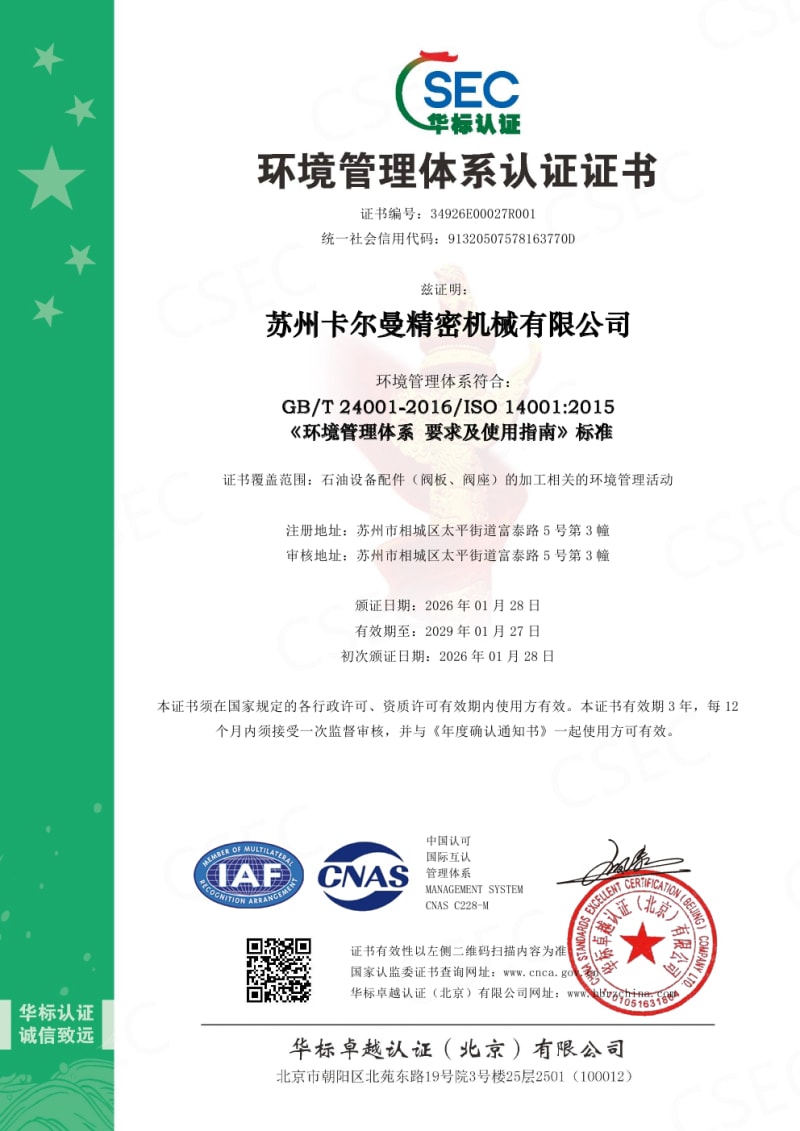
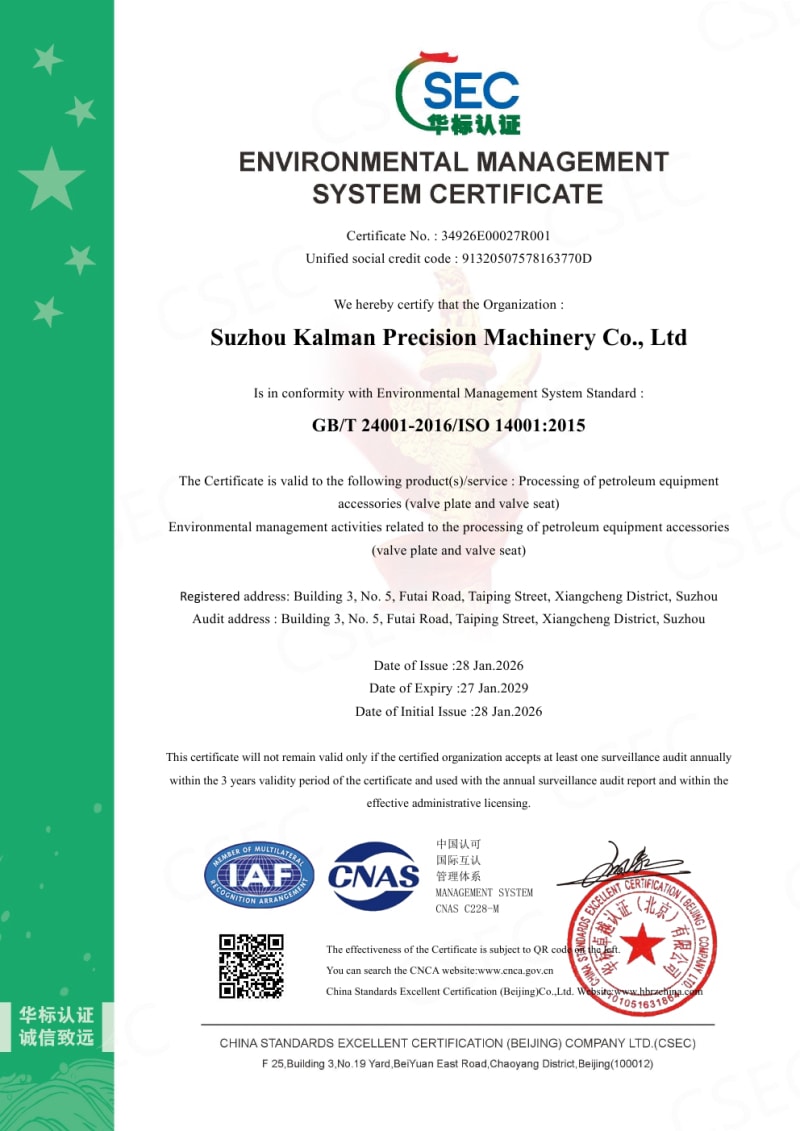
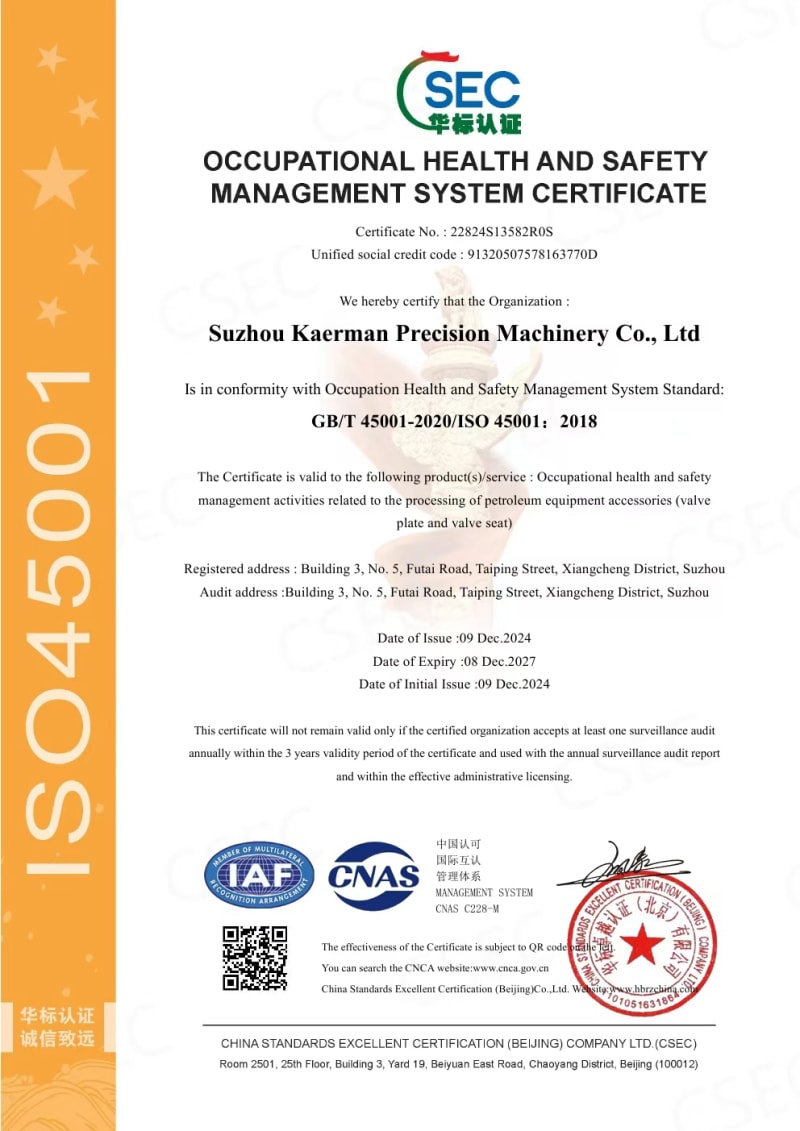
Explore our full range of precision-manufactured components, compatible with major US industry standards.